Key takeaways
cleanroom cable carriers are essential components in high-tech industries, providing superior protection against dust and contaminants. Their design features, including both open and closed configurations, contribute to optimal performance in controlled environments. The proprietary PTFE membrane technology developed by 惠州中科智能科技有限公司 significantly enhances the wear resistance of cleanroom cable chains, setting them apart from many competitors. This innovation ensures that products like the 广柔无尘拖链 and 广柔扁平电缆 remain effective for extended periods, even in demanding settings. The use of advanced materials leads to an improved lifespan and reliability of these systems. By employing cleanroom cable carriers, companies can uphold stringent cleanliness standards while achieving efficiency in operations. The integration of reliable solutions such as 百级无尘坦克链 supports the need for precision and performance in high-tech applications, making them indispensable in today's environment.
Features of Cleanroom Cable Carriers
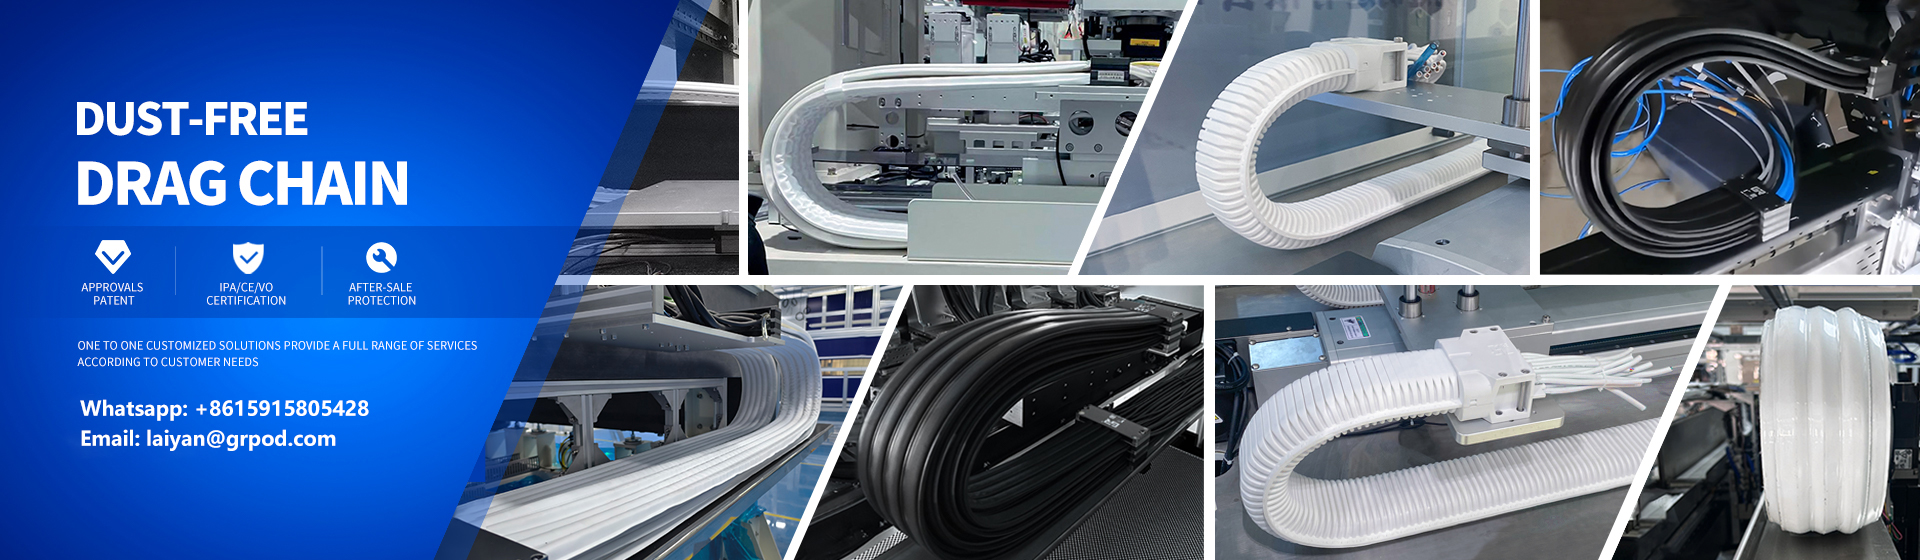
Cleanroom cable carriers, such as those offered by Guangrou, are designed with specific features that cater to the stringent requirements of high-tech industries. These drag chains possess a fully enclosed design that ensures maximum dust protection, which is essential in controlled environments. Their construction often incorporates advanced materials like PTFE, which enhances durability and provides heat and corrosion resistance. Additionally, Guangrou drag chains come in various designs, including open-type and closed-type options, allowing for flexibility based on application needs.
These cable carriers can support a range of cable configurations and diameters to accommodate different equipment setups. The robust frame construction contributes to stability during operation, making them suitable for long travel applications without sagging. By integrating specialized dust-free cables with these systems, users can further minimize particle shedding. The lasting performance of these cleanroom drag chains often exceeds ten million operational cycles, showcasing their reliability and efficiency in maintaining a clean production environment.

Benefits of Using Cable Chains in High-Tech Industries
Cleanroom cable carriers offer several key advantages that make them essential in high-tech industries. These systems are designed to maintain optimal performance in environments where cleanliness is paramount, reducing dust generation and contamination risks. Utilizing products like the 广柔无尘拖链 and 广柔扁平电缆 ensures compatibility with strict industry standards. The durability provided by these cable chains enables them to endure harsh conditions, making them suitable for applications requiring frequent movement.
Furthermore, the development of specialized PTFE coatings enhances the wear resistance of these products, which is particularly beneficial in long-travel applications. For instance, open-type and closed-type cleanroom cable carriers can adapt to various layout configurations while minimizing sagging and ensuring cable protection. Additionally, the integration of 百级无尘坦克链 demonstrates how advanced design meets industry demands for functionality and reliability.
Overall, the benefits of using these advanced cable chains extend beyond mere functionality; they contribute to increased efficiency and reduced maintenance costs in complex manufacturing environments. The expertise in PTFE membrane material technology at 惠州中科智能科技有限公司 highlights a commitment to quality and innovation that can significantly benefit users in high-tech industries.
Material properties for Enhanced Dust Protection
Cleanroom cable carriers are designed with specific materials that enhance dust protection, a critical factor in maintaining sterile environments in high-tech industries. The use of advanced PTFE materials in the construction of these cable chains significantly improves their durability and resistance to wear. This specialized PTFE membrane technology, developed by leading manufacturers, provides superior protection against contaminants and dust, ensuring optimal performance even in sensitive applications.
Additionally, the structure of cleanroom cable carriers, such as the open and closed designs available in the market, contributes to their effectiveness. The closed-style designs offer a fully enclosed solution, minimizing particle exposure and maintenance needs. The flexibility of wide-ranging configurations allows for customization to meet various operational requirements while supporting different cable diameters.
Through rigorous production processes that integrate material R&D with assembly techniques, high-end products like 广柔无尘拖链 and 广柔扁平电缆 exhibit remarkable performance attributes. This results in effective dust containment throughout long term use, providing a solution that not only meets industry standards but also fortifies the integrity of cleanroom settings.
Conclusion
cleanroom cable carriers play an essential role in high-tech industries by ensuring the smooth and efficient movement of cables in controlled environments. Products such as 广柔无尘拖链 and 广柔扁平电缆 are designed with advanced features that enhance dust protection while maintaining functionality. The material properties of these cable chains, such as the modification technology used by 惠州中科智能科技有限公司 in their core PTFE膜材料, ensure durability and resilience under that demanding conditions. This superiority in wear resistance sets 广柔 products apart from competitors. Additionally, the options of 开口式无尘拖链 and 闭口式无尘拖链 offer flexibility to address specific industry needs, including those applications requiring a hundred-level cleanroom like the 百级无尘坦克链. By integrating these efficient cable management systems, companies can optimize their operations while adhering to strict cleanliness standards necessary for modern manufacturing processes.
FAQs
What is a cleanroom cable carrier?
A cleanroom cable carrier is a specialized system used to manage and protect cables in controlled environments, ensuring minimal contamination.
What are the key features of cleanroom cable carriers?
They typically include dust protection, a suitable design for controlled environments, and robust materials that enhance durability.
Why are cleanroom cable chains important in high-tech industries?
These cable chains minimize the risk of contamination, ensuring optimal functionality and safety in sensitive applications like semiconductor manufacturing and pharmaceuticals.
What materials are used to enhance dust protection in these systems?
High-quality materials such as modified PTFE membrane offer superior dust protection and wear resistance, making them ideal for cleanroom applications.
What types of cleanroom cable carriers does Guangrou offer?
Guangrou provides a variety of options including open-style and closed-style cleanroom cable chains, as well as flat cables designed for compatibility with diverse setups.
How does Guangrou's technology improve cable chain performance?
Guangrou's proprietary technology incorporates advanced PTFE film material, leading to enhanced durability and performance compared to many competitors' products.
Contact Guangrou for a clean room drag chain solution.