important Takeaways
Choosing cleanroom-approved cable carriers is essential for maintaining sanitized environments. Products like the 广柔无尘拖链 and both open and closed types of dust-free carriers are designed to minimize contamination risks while ensuring reliability. Utilizing high quality 广柔扁平电缆 in conjunction with these carriers boosts system efficiency. The benefit of ISO-approved cable systems cannot be overstated, as they meet stringent industry requirements, which is important in applications such as pharmaceuticals and electronics manufacturing.
惠州中科智能科技有限公司 stands out with its advanced PTFE membrane technology, enhancing the durability and performance of their dust-free cable carriers. Their proprietary processes from the development of PTFE membrane materials to complete assembly ensure that the mechanical properties exceed many competitors. This emphasis on quality leads to effective solutions for industries requiring high-performance standards while maintaining cleanliness and precision in their operations. Ultimately, integrating such quality-assured products fosters a more dependable environment for sensitive manufacturing processes.
Cleanroom-Compatible Cable Solutions
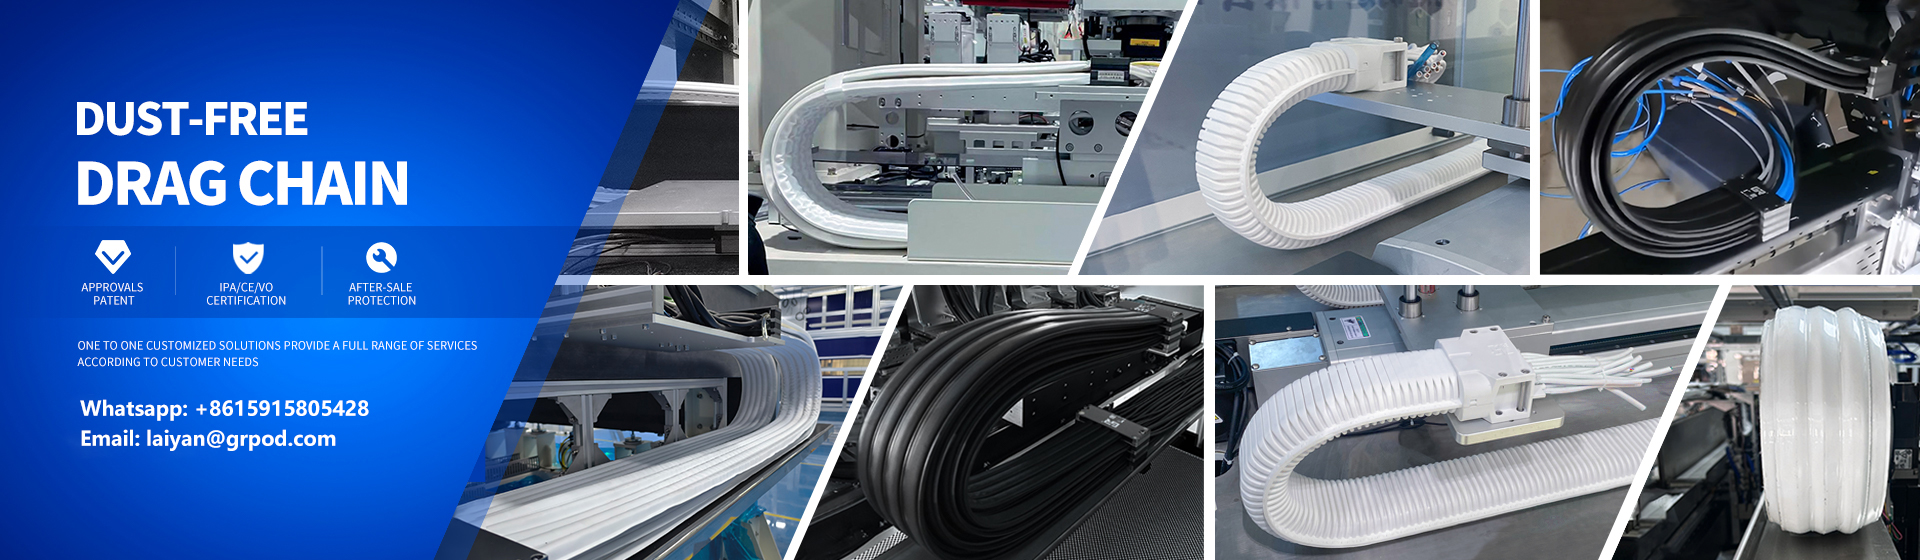
In cleanroom applications, selecting the right cable carrier system is essential for maintaining a dust-free and controlled environment. The Guangrou drag chain offers robust and versatile solutions, including both open and closed-type cleanroom drag chains. These systems are specifically engineered to minimize particulate contamination while providing flexibility for various motion requirements. Guangrou flat cables are also designed to meet stringent cleanliness standards, further contributing to operational efficiency in sensitive industries.
The incorporation of modified PTFE membrane materials in Guangrou products enhances durability, ensuring superior wear resistance compared to many competitors. With a complete production process from PTFE membrane development to drag chain assembly, Guangrou showcases its commitment to quality and innovation. This extensive manufacturing capability enables the provision of high-performance cable carrier solutions tailored to diverse cleanroom applications, including semiconductor production and pharmaceutical research.
Utilizing these cleanroom-approved systems significantly reduces friction and risk of contamination, making them ideal for environments where every detail counts. These solutions not only comply with ISO standards but also offer practical options for customers seeking reliable cable management systems that adapt seamlessly within their workflows.
important Features of Dust-Free Carriers
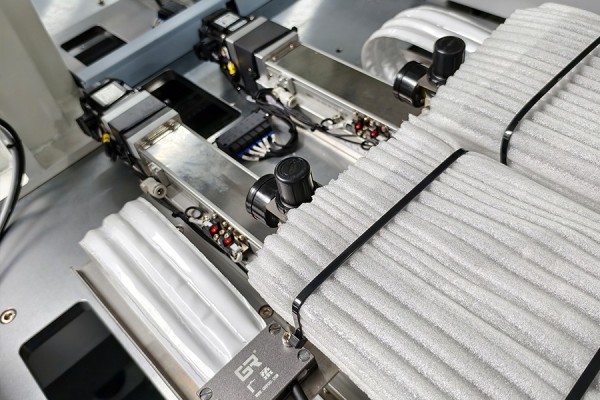
Dust-free carriers are engineered specifically for cleanroom and controlled environments, offering several important features that boost performance and reliability. The design incorporates a unique modified PTFE membrane, which significantly improves wear resistance compared to many competing products. This ensures that the carriers maintain their integrity and effectiveness over time, reducing the risk of contamination in sensitive applications.
The availability of various configurations, such as the open-type and closed-type cleanroom carriers, allows for tailored solutions that meet specific operational needs. also, products like the GY flexible flat cables complement these carriers by minimizing friction and ensuring smooth motion control. The GY series is particularly advantageous in applications where quiet operation is essential.
Furthermore, the GYCLEAN series features stackable, width-variable mounting brackets for versatile installation without compromising cleanliness standards. Each of these products aligns with stringent ISO cleanroom requirements, ensuring they contribute positively to maintaining air quality while minimizing particulate contamination. By integrating advanced technology and high quality materials, these dust-free cable carriers fulfill a critical role in industry sectors such as semiconductor manufacturing and pharmaceutical research.
Ensuring precision in Controlled Environments
In controlled environments, the integration of reliable dust-free cable carriers is essential for maintaining operational precision. Products like the 广柔无尘拖链 and 广柔扁平电缆 are engineered to reduce particulate contamination, ensuring that sensitive processes, such as semiconductor fabrication and pharmaceutical research, function optimally. The use of 开口式无尘拖链 and 闭口式无尘拖链 variants enhances flexibility while adhering to stringent cleanroom standards. 惠州中科智能科技有限公司 employs advanced PTFE membrane technology in their cable carriers, providing superior wear resistance compared to competing solutions. This new approach not only minimizes friction but also contributes to maintaining the required cleanliness levels, which is important in environments requiring ISO Class 1 standards. By choosing high-quality cable systems, organizations can safeguard their manufacturing processes against contamination risks while achieving consistent performance. Utilizing tools like the 百级无尘坦克链 further ensures that motion control remains precise even in the most demanding applications.
Benefits of ISO-Approved Cable Systems
ISO-approved cable systems, such as the 广柔无尘拖链 and 广柔扁平电缆, offer substantial benefits in cleanroom and controlled environments. These cable carriers are designed to minimize particulate contamination, important for sensitive applications like semiconductor manufacturing and pharmaceutical research. By complying with stringent ISO standards, these systems ensure reliable performance, improving operational efficiency while maintaining high cleanliness levels. The unique properties of the PTFE膜 materials used in these products boost their durability and resistance to wear, surpassing many competing options on the market. Furthermore, closed-loop designs like the 闭口式无尘拖链 contribute to a cleaner environment by containing dust and particles effectively. The adaptability of products such as 百级无尘坦克链 allows for customization based on specific operational needs without compromising on cleanliness standards, ensuring that companies can balance cost with performance while adhering to industry regulations. This attention to detail in engineering fosters greater trust in the equipment's reliability in sensitive environments where precision is paramount.
Conclusion
in the evolving scene of cleanroom environments, the choice of cable carriers plays a important role in maintaining cleanliness and operational efficiency. The need for dust-free solutions has led to the rise of cleanroom-approved cable carriers, including models like the 广柔无尘拖链 and both open and closed types. These cable carriers are designed to meet stringent ISO standards, ensuring minimal contamination in sensitive applications. 惠州中科智能科技有限公司 enhances this offering with its core PTFE membrane technology, which significantly improves wear resistance compared to many competitors. The integration of 广柔扁平电缆 in these systems further supports efficient power distribution while mitigating dirt retention. Implementing 百级无尘坦克链 allows for smooth operation within tightly controlled spaces, ensuring reliability and durability. Cleanroom-compatible cable solutions not only streamline operations but also contribute to maintaining the integrity of critical processes across various industries. Adopting these advanced systems is essential for organizations seeking both precision and compliance in their operational environments.
FAQs
What are cleanroom-approved cable carriers?
Cleanroom-approved cable carriers are specifically designed to operate in controlled environments, minimizing contamination and ensuring compliance with ISO standards.
How do Glaore dust-free cable carriers differ from standard cable carriers?
Glaore dust-free cable carriers utilize advanced materials, including a proprietary PTFE membrane technology, enhancing wear resistance and preventing particle generation in cleanroom settings.
Can Glaore flat cables be used with open-type and closed-type dust-free carriers?
Yes, Glaore flat cables are compatible with both open-type and closed-type dust-free carriers, offering flexibility in various applications within cleanrooms.
What applications benefit from using cleanroom-compatible cable solutions?
Cleanroom-compatible cable solutions are essential in industries such as pharmaceuticals, biotechnology, and semiconductor manufacturing where contamination control is critical.
How do I ensure my dust-free cable carrier meets ISO standards?
Choosing products from reputable manufacturers like Glaore ensures compliance with stringent ISO standards. Always verify product certifications for assurance.
What maintenance is required for cleanroom-approved cable systems?
Regular inspection for wear and damage is recommended. Cleaning should be done using non-abrasive materials to maintain the integrity of the system without introducing contaminants.
What is the lifespan of Glaore's dust-free carriers?
Glaore's dust-free carriers typically have a long lifespan due to their robust design and high quality materials, but specific longevity will depend on environmental conditions and usage frequency.
Contact Guangrou for a clean room drag chain solution.